| Quantity: | |
|---|---|


Trehalose
Organic Trehalose is a high-quality, naturally occurring disaccharide composed of two glucose molecules linked together. Recognized for its exceptional stability and functional versatility, it has become a highly sought-after ingredient in the modern food formulation industry. Unlike conventional sugars, trehalose provides unique physicochemical properties that go beyond basic sweetening. It is widely utilized by manufacturers for its remarkable ability to ensure moisture retention and comprehensive food stabilization.
As consumer demand shifts toward healthier, clean-label options, this natural sweetener stands out by enhancing flavor profiles and maintaining the structural integrity of food products. By preventing moisture migration and protecting sensitive components during manufacturing, Organic Trehalose serves as an essential functional ingredient for businesses aiming to elevate product quality, extend shelf life, and meet the rigorous standards of today's health-conscious market.

One of the most critical properties of Organic Trehalose is its superior moisture retention capability. At a molecular level, it forms strong hydrogen bonds with water, effectively trapping moisture within the food matrix. This mechanism is crucial for maintaining the intended texture, mouthfeel, and overall freshness of the final product. By significantly reducing water activity and preventing moisture loss, this disaccharide helps mitigate common issues such as staling, drying out, or unwanted crystallization over time. For manufacturers, this translates to a more stable product that retains its premium quality throughout an extended shelf life, ultimately reducing waste and enhancing consumer satisfaction.
Beyond moisture control, Trehalose acts as a highly effective food stabilization agent. It possesses a unique ability to protect sensitive ingredients—such as proteins and lipids—from degradation during harsh processing conditions and prolonged storage. Whether subjected to extreme temperature fluctuations, freezing, or dehydration, trehalose forms a protective glassy matrix that prevents cellular damage and protein denaturation. This stabilization process is vital for preserving the original taste, color, texture, and visual appearance of processed foods. By incorporating this ingredient, formulators can ensure that their products maintain structural integrity and sensory appeal from the production line to the consumer's table.
Functioning as a premium natural sweetener, Organic Trehalose offers a clean, mild sweetness profile that is approximately 45% as sweet as sucrose. This gentle sweetness enhances and balances natural flavors without overpowering them, allowing the authentic taste of the core ingredients to shine. More importantly, it aligns perfectly with the growing market trend toward healthier nutritional profiles. Trehalose provides a functional alternative without the high caloric impact typically associated with traditional sugars. This makes it an indispensable ingredient for developing low-calorie diets and sugar-free products. Manufacturers can leverage this natural sugar to create innovative, healthier alternatives that do not compromise on flavor, texture, or overall eating experience.
When sourcing functional food ingredients, partnering with a reliable supplier is paramount. At ZIO Chemical, we specialize in providing high-quality Organic Trehalose that strictly adheres to international food safety and quality standards. With over 25 years of experience in the food additive industry, our team possesses the deep technical expertise required to support your manufacturing goals.
We pride ourselves on delivering cost-effective, safe, and highly reliable solutions tailored to the needs of modern food production. Our premium trehalose is the perfect choice for manufacturers striving to expand their portfolios with sugar-free, low-calorie, and health-conscious options. By choosing ZIO Chemical, you are guaranteed not only superior product purity but also timely delivery, consistent supply chain stability, and comprehensive technical support to ensure your formulation success.
The following table outlines the standard packaging specifications, shelf life, and recommended storage conditions for our Organic Trehalose. These parameters are provided to support efficient logistics, proper inventory management, and long-term product stability for bulk purchasing requirements.
| Attribute | Detail |
|---|---|
| Name | Trehalose |
| Ingredient | Trehalose |
| Specification | 25kg |
| Capacity | 20 kg |
| Place Of Production | Guangzhou, China |
| Shelf Life | 2 years |
| Storage Conditions | Store in a cool, dry place away from direct sunlight and moisture. Best storage temperature: 20°C to 25°C (68°F to 77°F). |


Incorporating Organic Trehalose into your production formulations is a proven strategy to elevate the overall quality, texture, and taste of premium food products. For frozen applications such as ice cream, it acts as a highly effective cryoprotectant. By managing water activity and controlling freezing points, it significantly reduces the formation of undesirable ice crystals during temperature fluctuations and freeze-thaw cycles. This ensures the rich, consistently smooth, and creamy texture that consumers expect. Furthermore, its mild sweetness—only about 45% that of sucrose—allows the authentic flavors of your ingredients to shine without being overly sweet. Whether used in delicate dairy products, artisanal baked goods, or complex savory sauces, it helps ensure that your products maintain their intended mouthfeel, structural integrity, and premium consistency, even after prolonged storage.
For commercial food manufacturers, shelf stability is directly linked to profitability. By effectively retaining moisture and stabilizing protein and lipid structures, Trehalose naturally extends the shelf life of a wide array of food products. It provides a unique protective barrier against environmental stressors, preventing moisture loss that leads to staleness and inhibiting lipid oxidation that causes off-flavors. This protective mechanism is particularly beneficial for extending the longevity of items like snacks, candies, and various processed foods. By maintaining product freshness and visual appeal for longer periods, businesses can significantly reduce food waste, lower return rates, and confidently expand their distribution radius, ultimately improving overall supply chain efficiency.
Trehalose is highly versatile and seamlessly adapts to numerous manufacturing environments, making it an invaluable tool for R&D teams looking to upgrade their product portfolios. Its exceptional stability under high heat and low pH conditions means it will not degrade during rigorous processing.
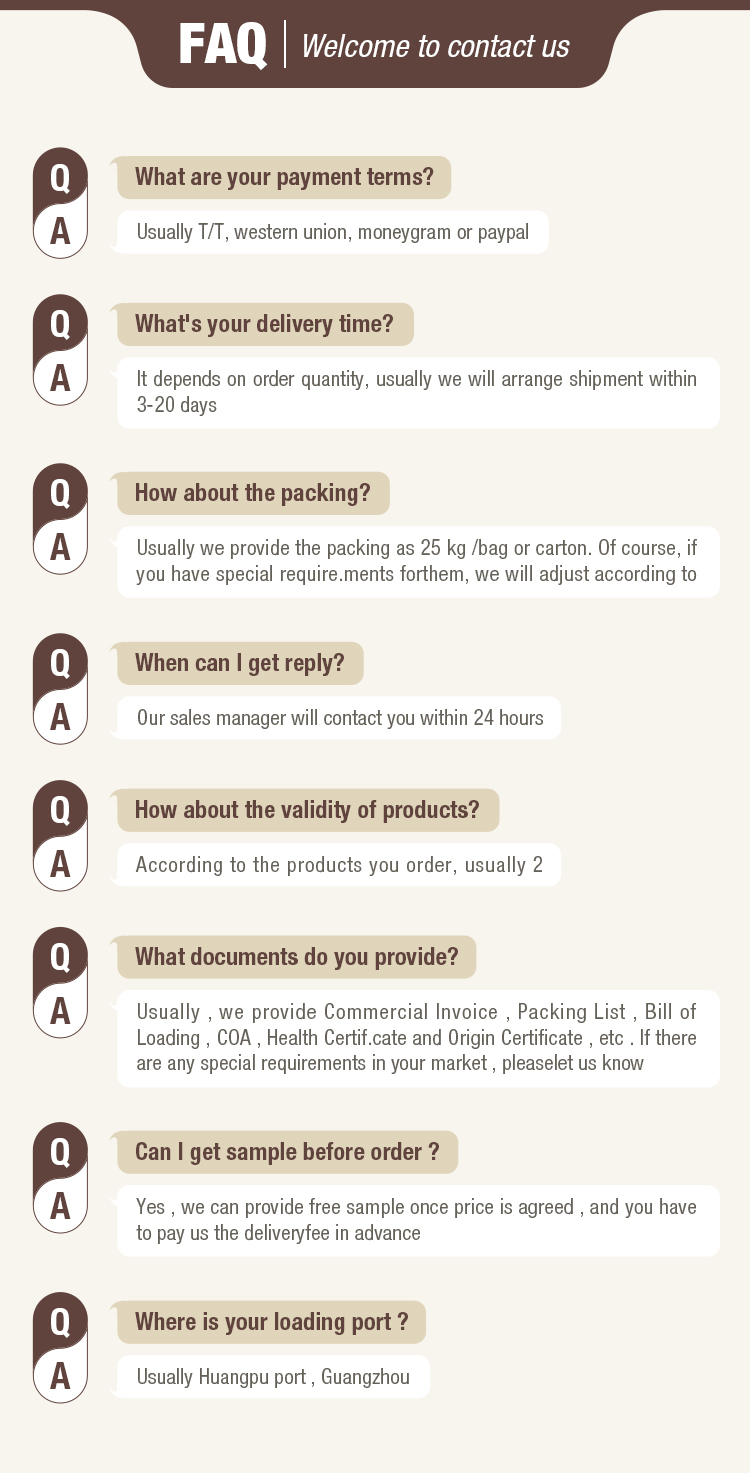
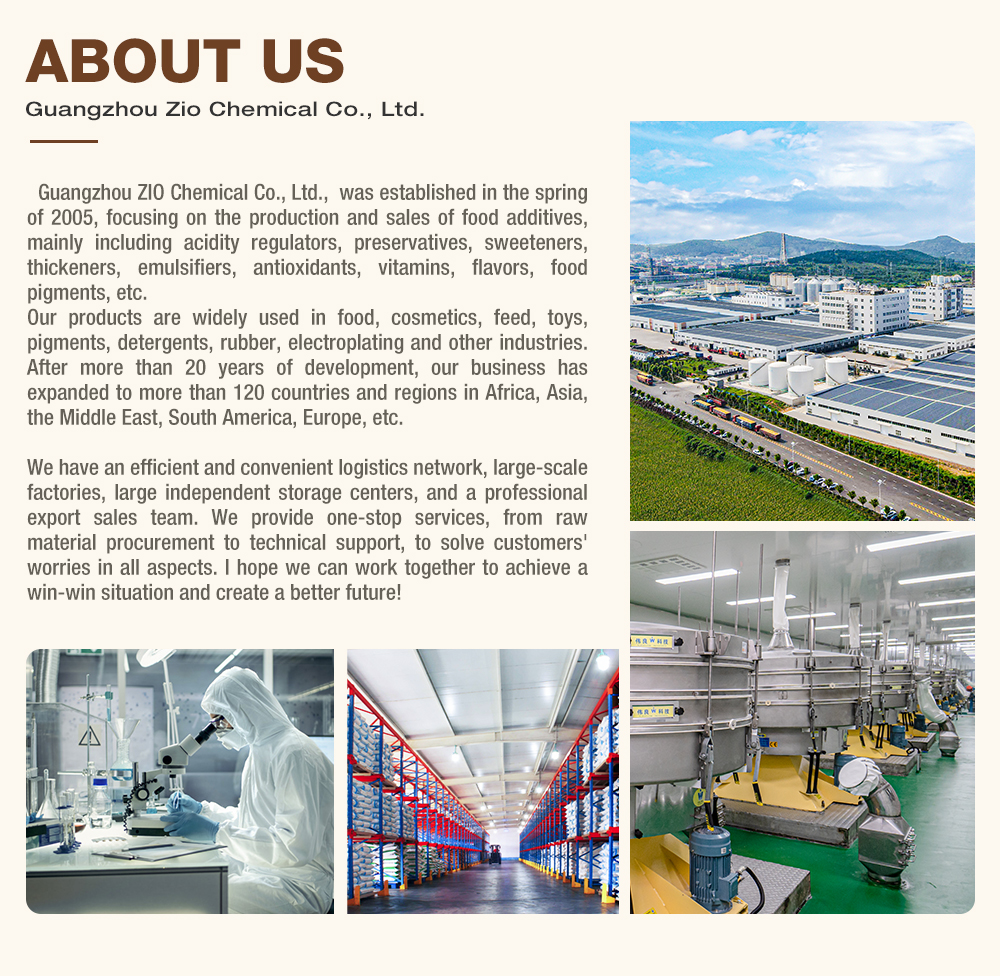
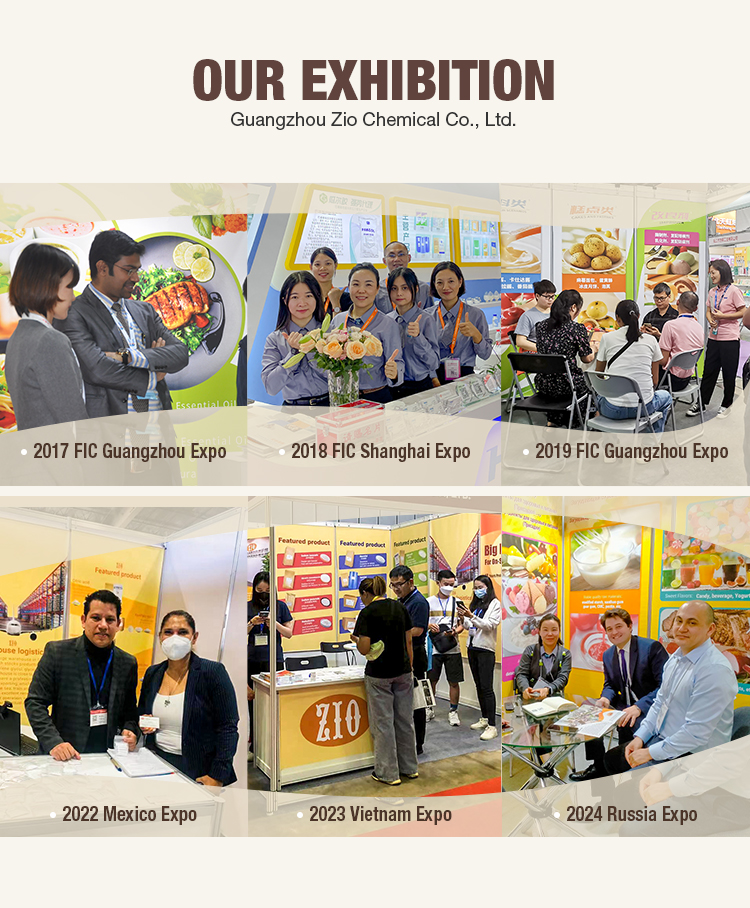
As a dedicated partner in the food ingredient industry, we back our high-quality products with robust manufacturing capabilities, stringent quality control, and a reliable global supply chain. From advanced production facilities and strict certification standards to professional logistics and active participation in international exhibitions, we are fully equipped to meet your large-scale procurement needs securely and efficiently. Explore our comprehensive operational strength through the gallery below.


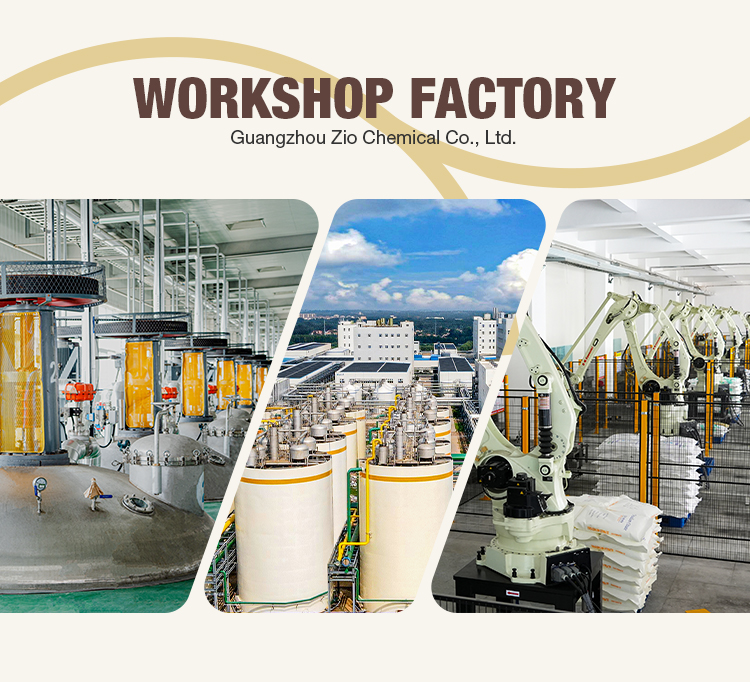


Please review the visual guide below for frequently asked questions regarding the procurement, lead times, and application details of our Organic Trehalose for Ice Cream.