| Quantity: | |
|---|---|


Potassium Sorbate is widely recognized as a highly effective and dependable food preservative, serving as a critical ingredient for food and beverage manufacturers worldwide. Its primary function lies in its exceptional ability to inhibit the growth and reproduction of mold, yeast, and various spoilage microorganisms. By neutralizing these biological threats, Potassium Sorbate significantly extends the shelf life of perishable goods without altering their natural taste, color, or aroma. For food processors, integrating this preservative means ensuring that products maintain their original quality and nutritional value from the production facility all the way to the consumer's table. It provides a reliable safeguard against premature spoilage, helping brands uphold their reputation for consistency and safety over time.

The core value of Potassium Sorbate lies in its robust preservation capabilities, which directly translate to a significantly longer shelf life for a diverse array of consumables. By creating an environment that actively suppresses yeast and mold proliferation, it effectively halts the degradation processes that lead to food spoilage. This is particularly crucial for moisture-rich products such as fruit juices, savory sauces, and baked goods, which are naturally highly susceptible to microbial growth. For manufacturers, utilizing this preservative drastically minimizes product waste, reduces the risk of returns, and allows for broader geographical distribution. The extended shelf life ensures that items remain fresh and visually appealing throughout their intended commercial lifespan.
One of the standout characteristics of this preservative is its remarkable versatility across the food and beverage industry. It is not restricted to a single category but serves as a universal preservation solution for a wide spectrum of food products. From sweet confections and baked pastries to complex dairy items and acidic sauces, Potassium Sorbate adapts seamlessly to various processing environments. Its excellent solubility makes it incredibly easy to incorporate into liquid mixtures, syrups, and marinades. This flexibility allows food scientists and manufacturers to streamline their ingredient sourcing, using a single, dependable preservative to protect multiple distinct product lines while maintaining strict formulation standards.
Beyond its primary role in preventing microbial spoilage, Potassium Sorbate also offers valuable functional benefits that enhance the overall physical quality of food products. When integrated into specific formulations, it contributes to improved texture and mouthfeel by supporting the formation of stable emulsions. In products prone to ingredient separation, such as certain dairy products and blended beverages, it helps maintain a uniform consistency. By preventing the unsightly separation of different phases, it ensures that the end product delivers a smoother, creamier, and more cohesive sensory experience. This structural stability not only improves the consumer's eating or drinking experience but also enhances the visual attractiveness of the product on the retail shelf.
Review the detailed technical specifications of our food-grade Potassium Sorbate below. These parameters are provided to help procurement teams and formulators verify product suitability, chemical composition, and shelf-life requirements for manufacturing needs.
| Attribute | Detail |
|---|---|
| Name | Potassium Sorbate |
| Ingredient | Potassium Sorbate (C₆H₇KO₂) |
| Specification | White crystalline powder (food grade) |
| Place Of Production | Guangzhou |
| Shelf Life | 24 months |
| Storage Conditions | Store in a cool, dry place away from sunlight |
Note for Storage and Handling: To ensure optimal preservation efficacy and maintain the full 24-month shelf life, please adhere strictly to the recommended storage conditions. Keeping the powder in a cool, dry environment protected from direct sunlight prevents degradation and supports stable inventory management.
When selecting Potassium Sorbate for preservation, purchasing managers and production directors prioritize stability, regulatory adherence, and overall value. Our commercial-grade preservation solution is precisely formulated to support food manufacturers in optimizing their production lines while maintaining strict quality control. The following commercial advantages highlight why this additive serves as a dependable choice for large-scale manufacturing, distribution, and long-term inventory management.
Our Potassium Sorbate is meticulously produced to comply with rigorous food additive standards, making it a highly safe choice for both manufacturers and end consumers. For procurement teams and compliance officers, sourcing a fully compliant preservative is critical to mitigating regulatory risks and ensuring smooth market entry across diverse domestic and international regions. Its established safety profile provides confidence that the final consumer goods remain safe for consumption over extended periods. By integrating a standardized preservation solution, food processing facilities can distribute their products globally without facing unexpected compliance hurdles, thereby ensuring continuous and uninterrupted supply chain operations.
Managing production overhead is a primary concern in the competitive food industry, and this preservative offers an economical solution for enhancing overall food quality and stability. It effectively improves shelf life without significantly increasing production costs, providing great value for food manufacturers aiming to balance quality with budget constraints. Integrating this additive into your existing formulation processes requires minimal operational adjustment while delivering substantial financial returns through prolonged product viability. This inherent cost-efficiency allows facilities to scale up production, optimize their supply chain economics, and ultimately improve overall operational profitability without compromising on safety.
Maintaining product stability from the manufacturing facility to the retail shelf is essential for protecting brand reputation and consumer trust. Potassium Sorbate actively helps reduce food waste by preventing premature degradation and spoilage during complex transit and storage phases. This reliable performance contributes directly to a longer shelf life and facilitates better quality control throughout the entire distribution network. By minimizing spoilage, food manufacturers can significantly decrease inventory loss, lower the risk of product recalls, and maximize their return on investment. A consistently stable product ensures that distributors and retailers receive goods in optimal condition, securing long-term commercial partnerships and repeat orders.
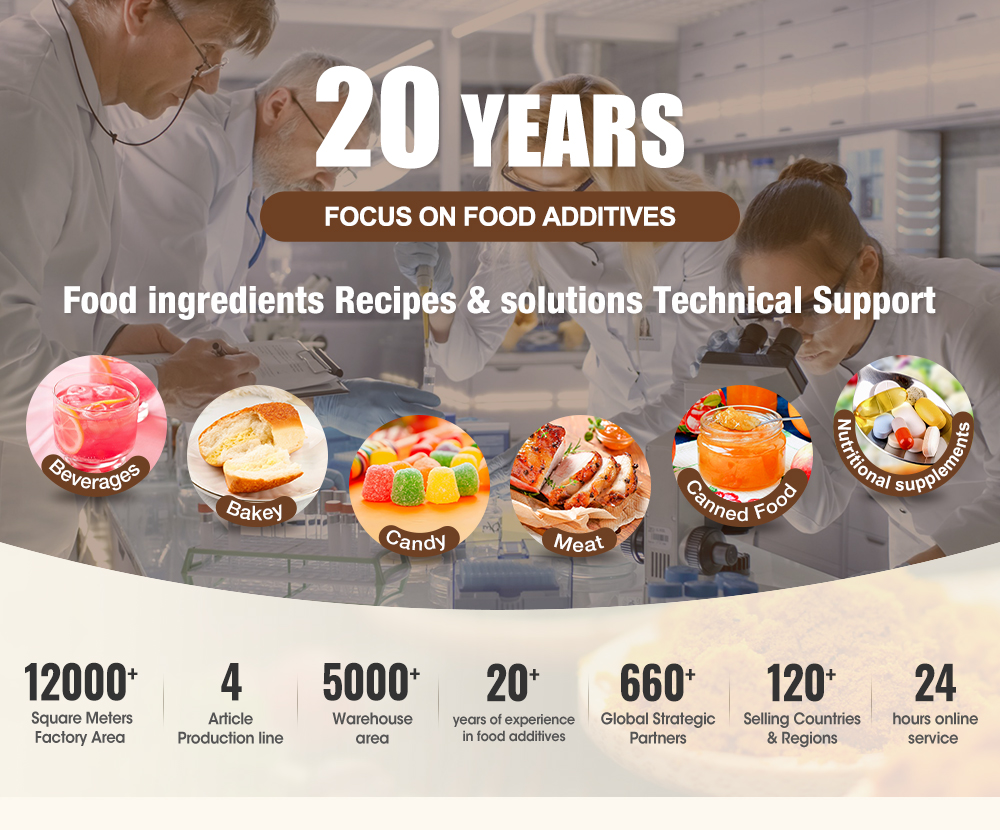
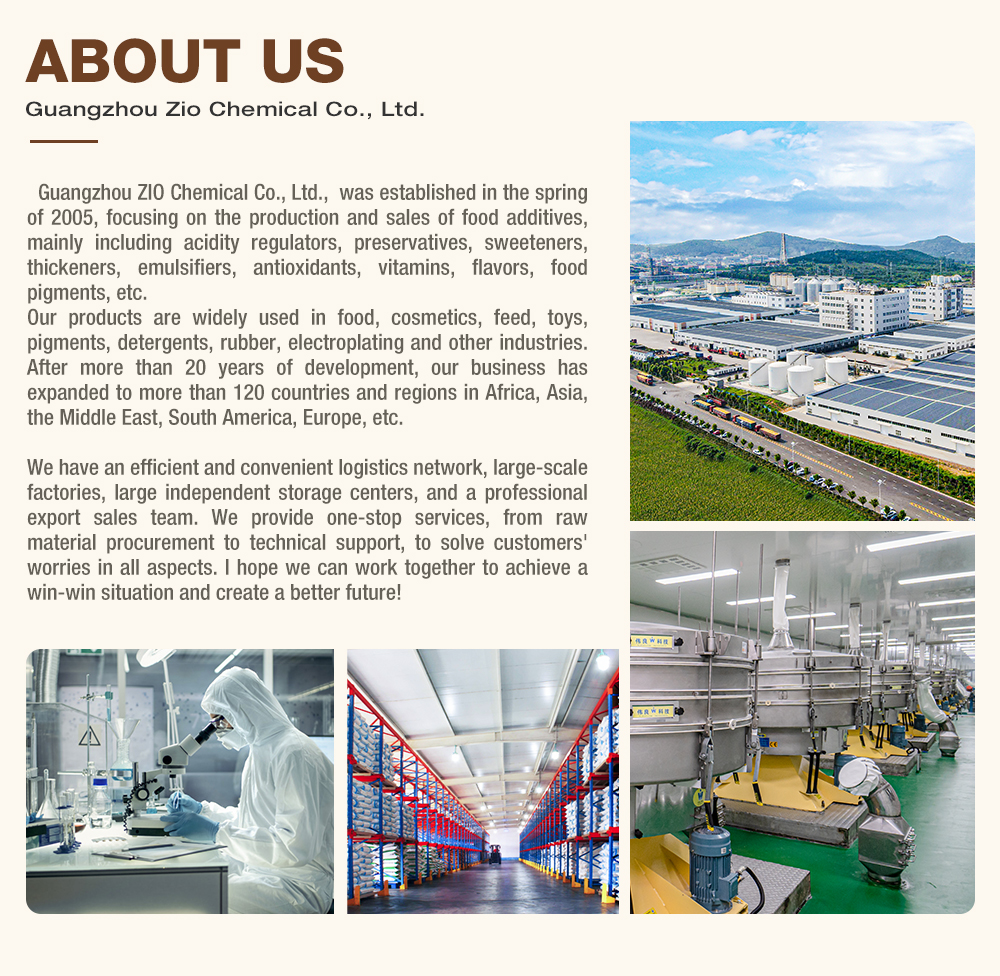
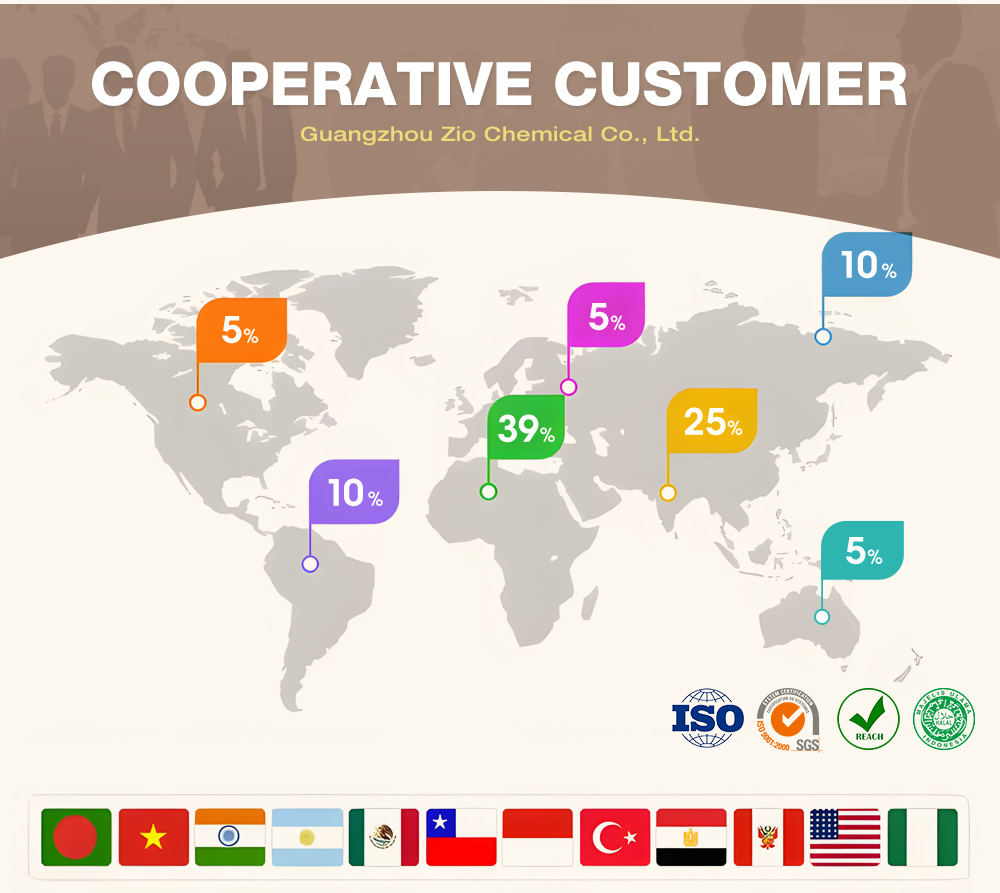
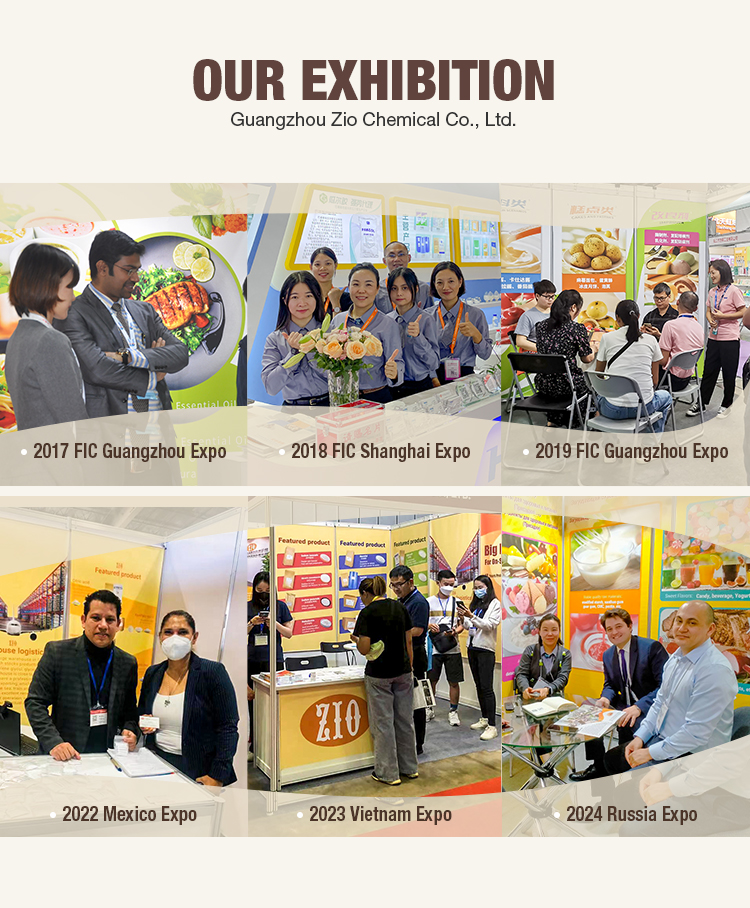
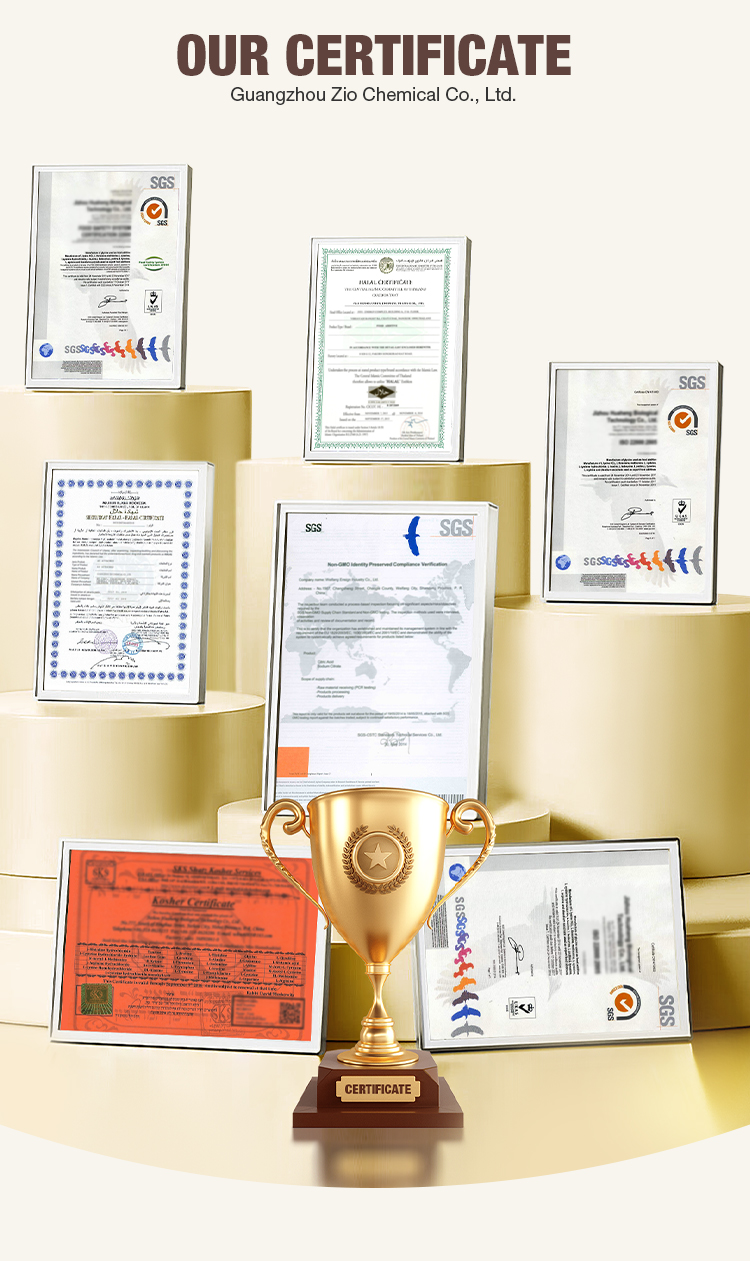
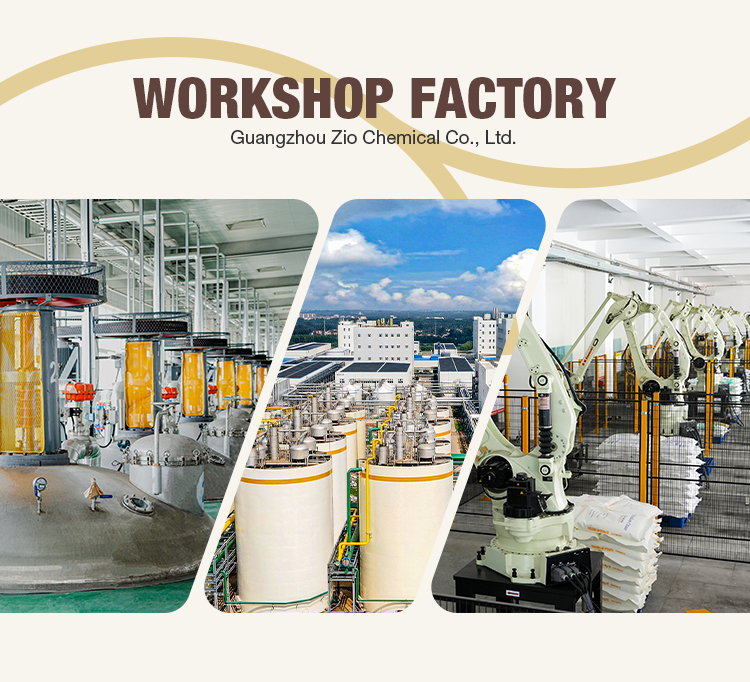
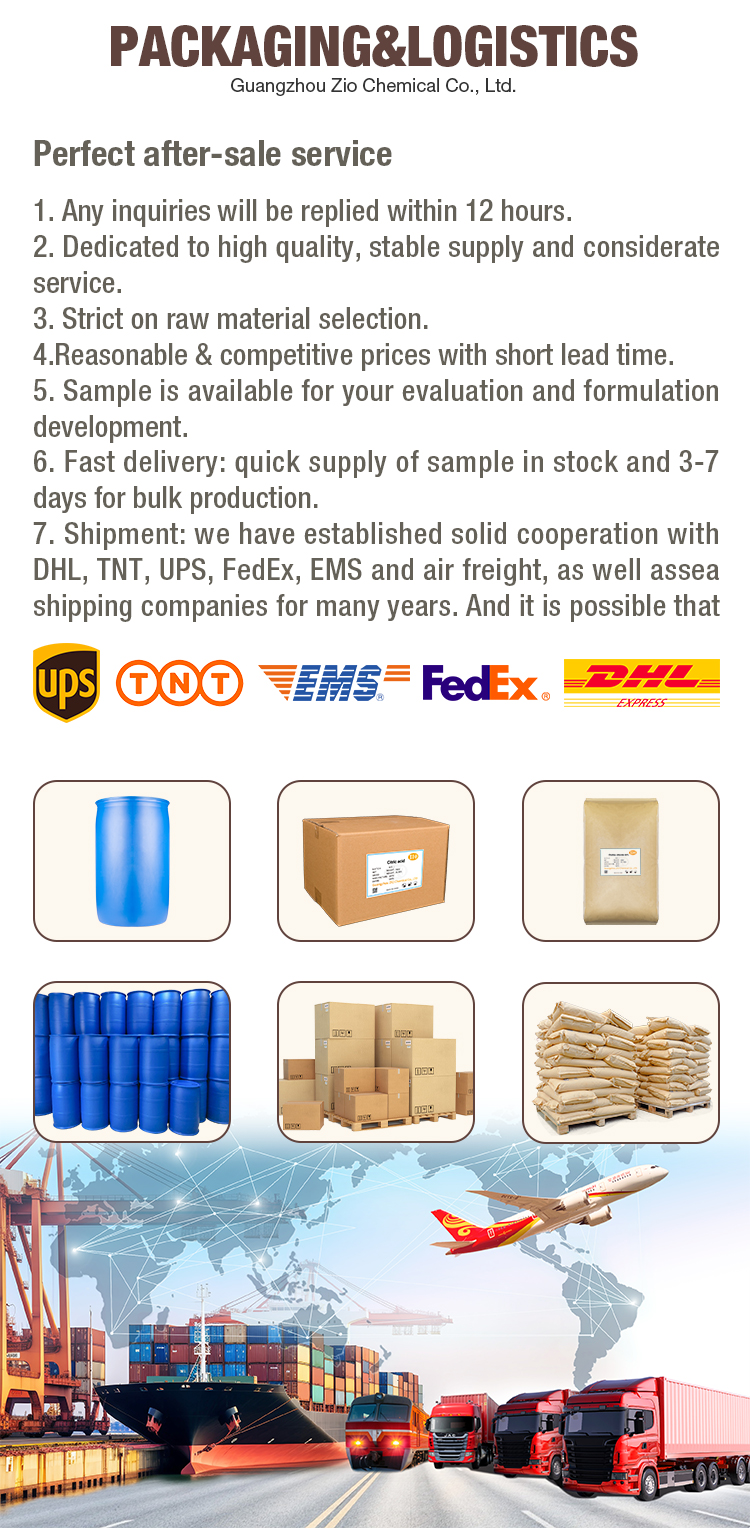
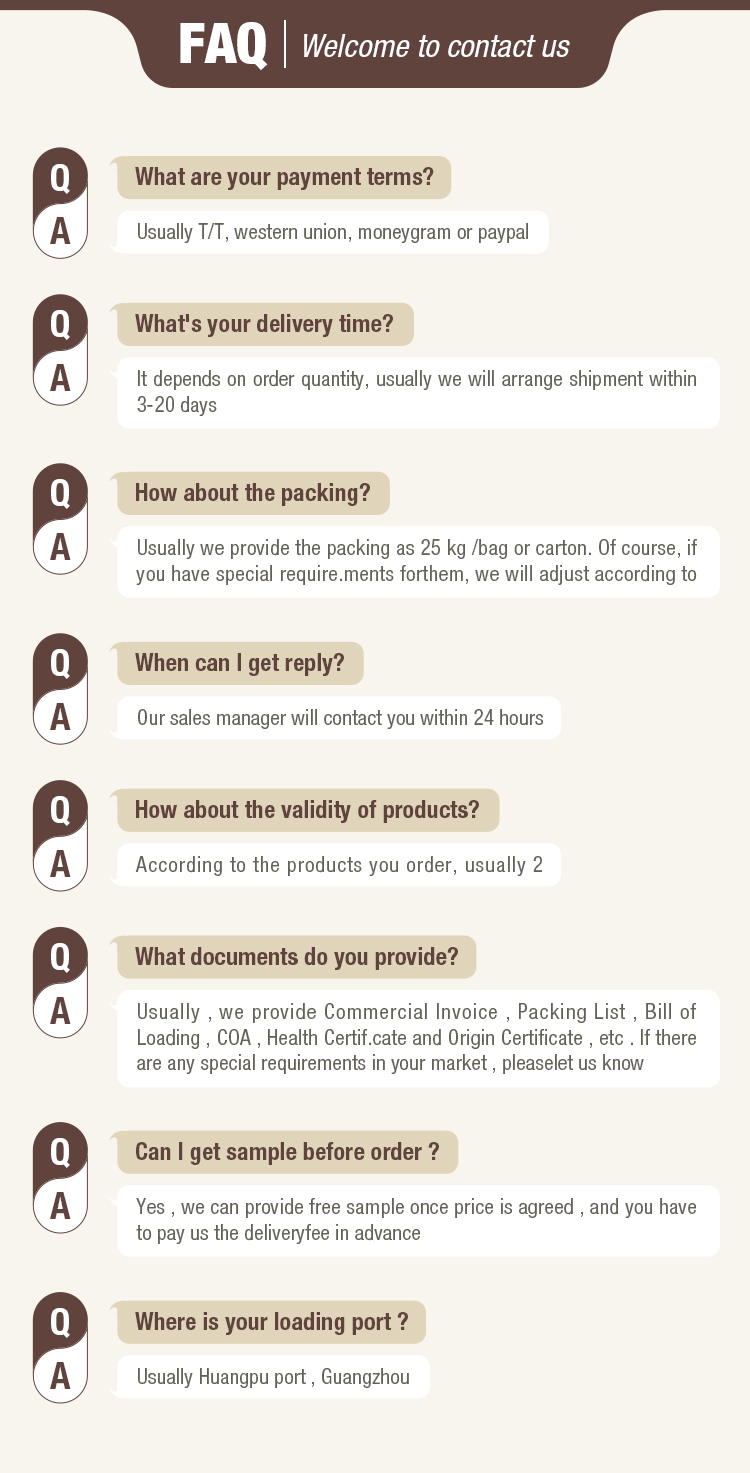
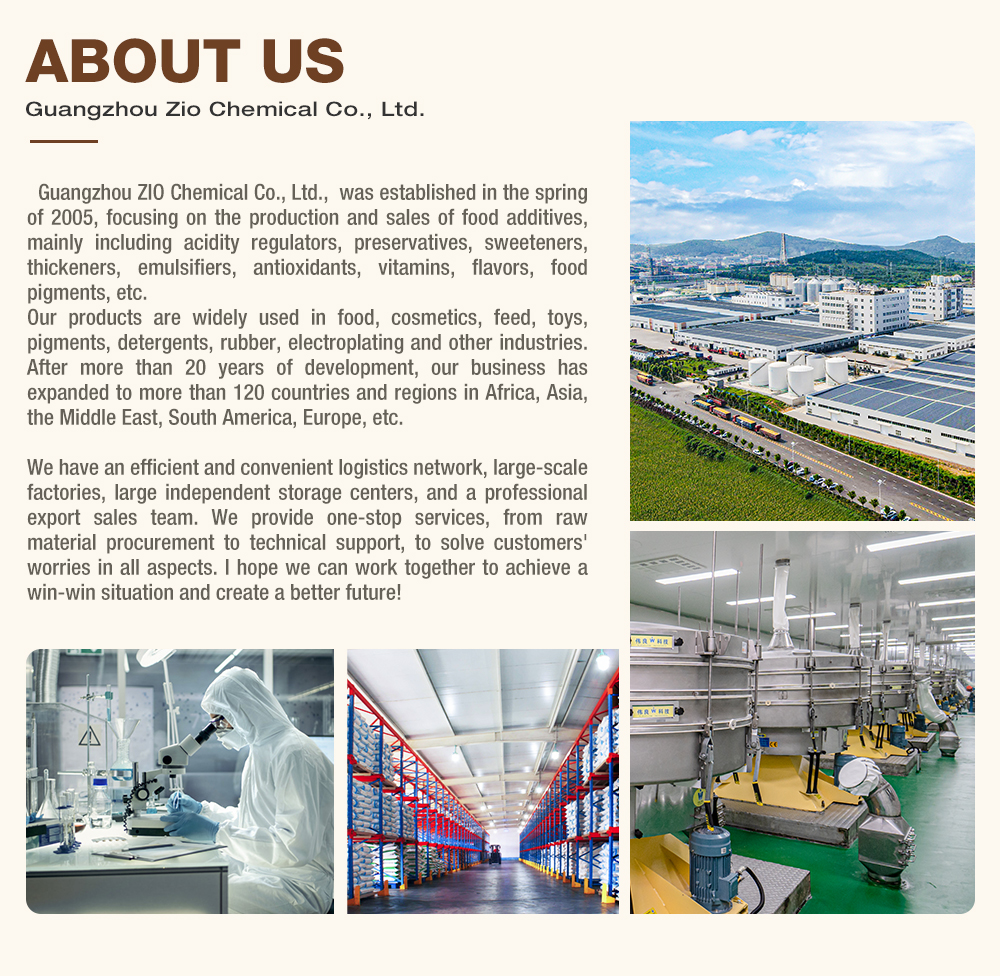
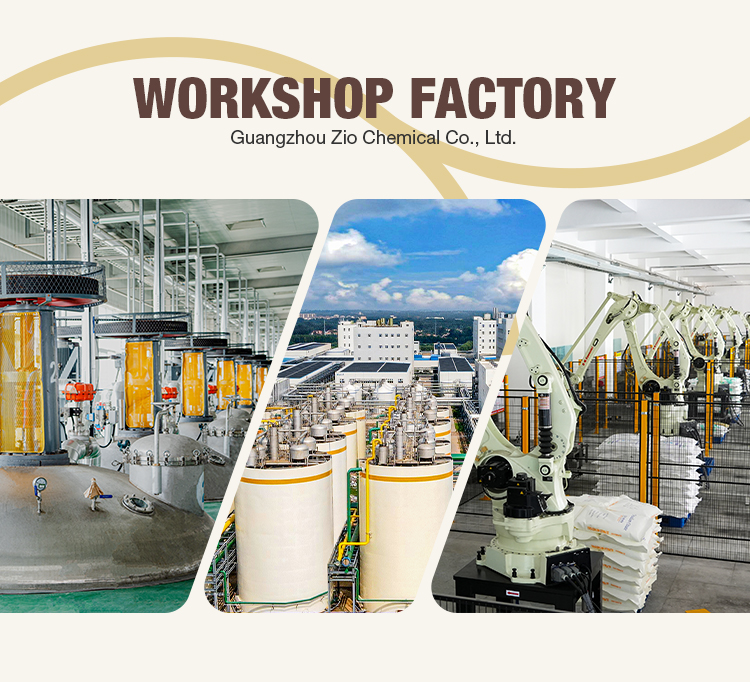
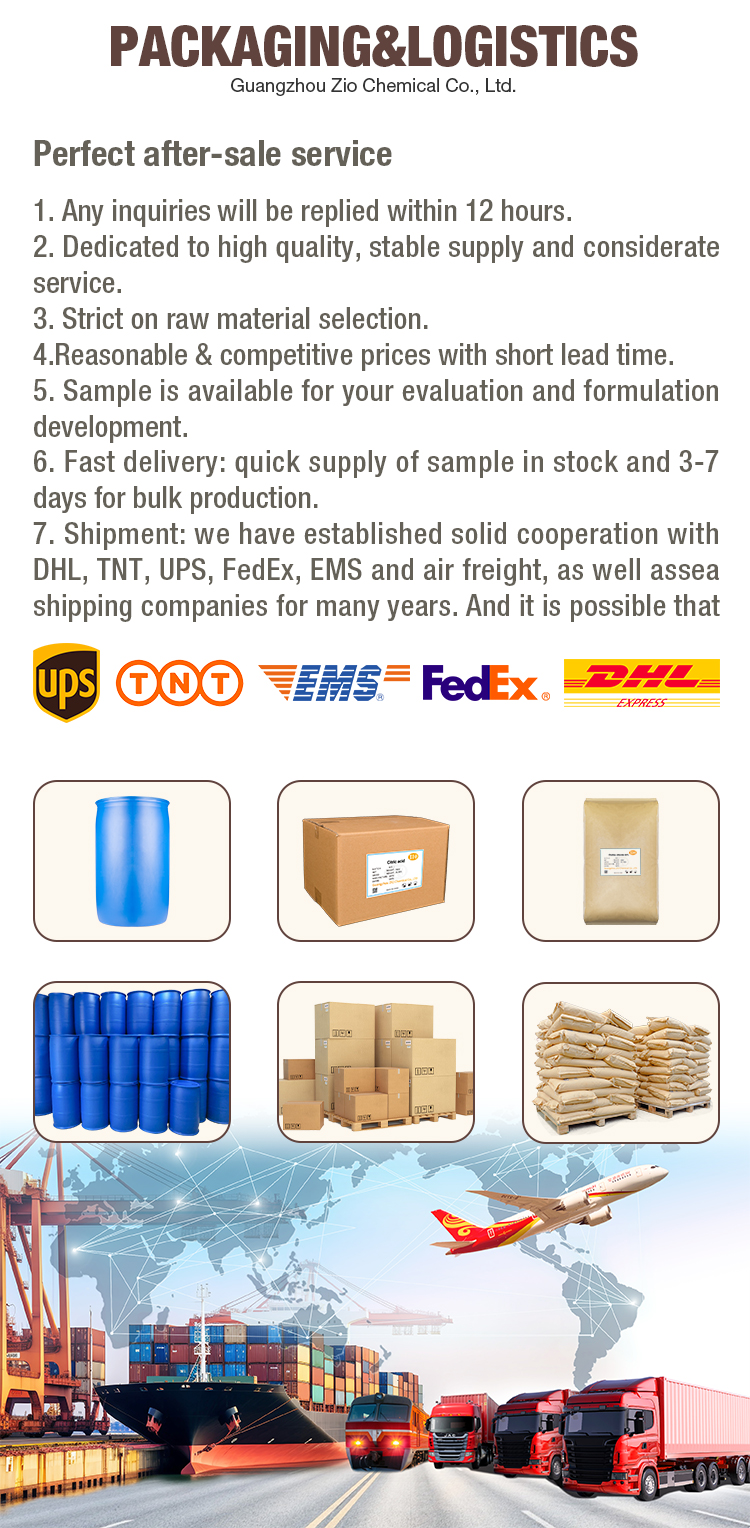
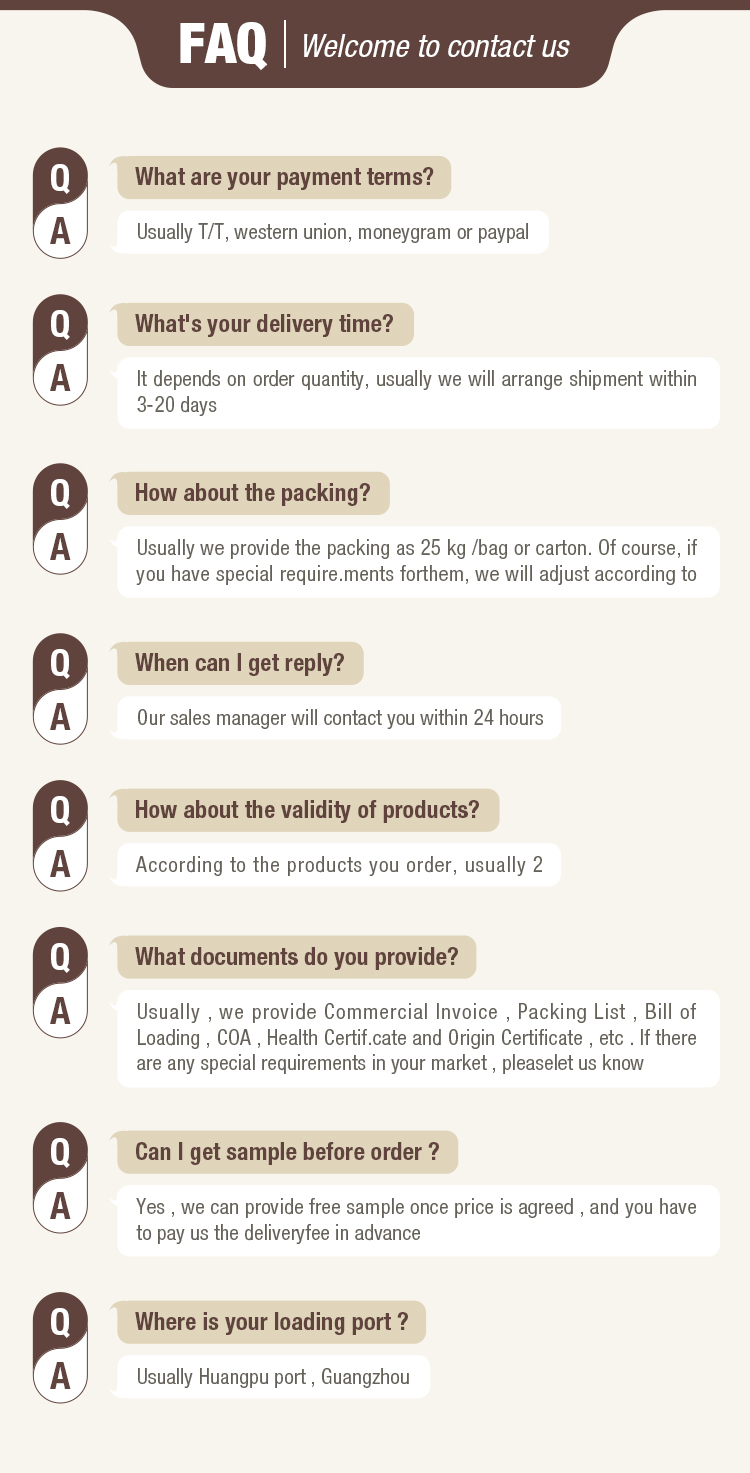
We understand that securing a reliable product requires backing by a robust supply chain, transparent manufacturing infrastructure, and comprehensive logistical support. Below is a detailed visual overview of our company facilities, production capabilities, industry certifications, and logistics framework, demonstrating our unwavering commitment to serving your complex procurement needs efficiently.



Q: What is the shelf life of this Potassium Sorbate?
A: The standard shelf life of our food-grade Potassium Sorbate is 24 months, provided it is kept under the recommended storage conditions.
Q: How should the product be stored to maintain its efficacy?
A: It must be stored in a cool, dry place. Ensure the packaging is tightly sealed to protect the preservative from moisture and direct environmental exposure.
Q: What types of products is this preservative suitable for?
A: It is widely applied in the food and beverage industry to effectively inhibit yeast and mold growth, thereby extending the product's shelf life safely and reliably.