| Quantity: | |
|---|---|


Microcrystalline Cellulose (MCC)
ZIO
Microcrystalline Cellulose (MCC) is a highly purified, multi-functional food-grade excipient and pharmaceutical excipient derived from natural plant cellulose. Manufactured through the controlled hydrolysis and rigorous purification of α-cellulose, it presents as a premium white, odorless, and tasteless crystalline powder. Recognized globally for its exceptional physical and chemical stability, MCC plays a critical role in various manufacturing processes. In the food sector, it functions as a highly effective stabilizer, thickener, and dietary fiber. In pharmaceutical manufacturing, it is widely utilized as a reliable tablet diluent, binder, and disintegrant. Its unique ability to significantly improve product texture, structural integrity, and processability makes it an essential raw material for formulation engineers and procurement specialists seeking consistent quality.
Beyond traditional food and pharmaceutical manufacturing, Microcrystalline Cellulose (MCC) is extensively adopted in the production of dietary supplements to ensure precise ingredient distribution and uniform formulation consistency. In the cosmetics industry, it acts as an advanced suspending agent and absorbent, providing a smooth, non-greasy feel in skincare and makeup formulations. Its universal compatibility with diverse active ingredients, combined with strict adherence to global pharmacopeia and food safety standards (including USP, EP, and FCC), ensures it effectively meets the complex demands of various applications, ranging from baked goods and dairy products to hard capsules, oral tablets, and nutritional powders.
Property | Description |
Chemical Name | Microcrystalline Cellulose |
Molecular Formula | C₆H₁₀O₅ₙ |
Appearance | White to off-white crystalline powder |
Odor | Odorless, tasteless |
Particle Size Range | 20μm – 200μm (customizable grades: MCC101, MCC102, etc.) |
Solubility | Insoluble in water and organic solvents, but dispersible |
Density | Approx. 1.5 g/cm³ |
Safety | Complies with USP, EP, FCC standards; safe and stable raw material |
Functional Properties | Excellent compressibility and binding ability |
Superior dispersibility and stability | |
Low hygroscopicity for easy storage | |
Good suspension and emulsification properties |
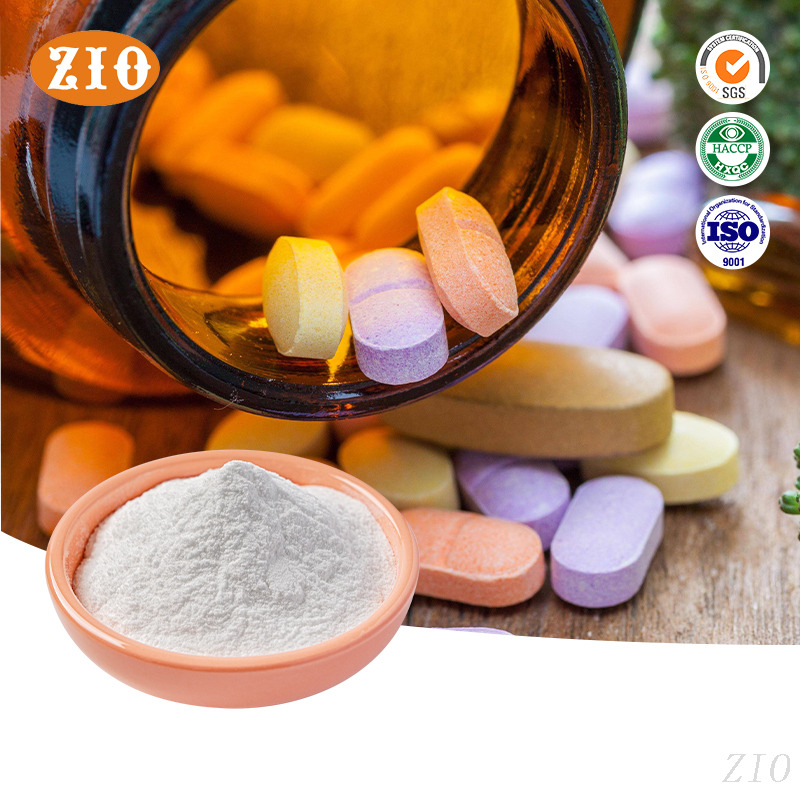
The fundamental active component of our Microcrystalline Cellulose (MCC) is high-purity α-cellulose, meticulously extracted from renewable natural plant sources such as wood pulp or cotton linters. This raw material undergoes a highly controlled acid hydrolysis process to strip away non-cellulosic impurities, followed by advanced purification techniques to isolate the desired crystalline structure. The complete absence of synthetic additives, artificial preservatives, or harmful residual solvents ensures that the MCC maintains its natural origin and exceptional safety profile. This purity minimizes the risk of adverse chemical reactions in complex formulations, making it a highly reliable choice for human consumption in both food and pharmaceutical products.
To support global procurement requirements and reduce formulation risks, every batch of Microcrystalline Cellulose (MCC) is rigorously tested to ensure full compliance with USP standards, EP standards, and FCC standards. This comprehensive quality control framework guarantees strict consistency in purity levels, precise particle size distribution, and dependable functional properties. Whether utilized as a food stabilizer, a pharmaceutical binder, or a nutritional supplement carrier, buyers can trust in its reliable, batch-to-batch performance.
In the highly regulated pharmaceutical sector, Microcrystalline Cellulose (MCC) delivers excellent compressibility, allowing manufacturers to produce robust, uniform tablets with consistent hardness and predictable dissolution profiles. Its superior dispersibility guarantees the even distribution of active pharmaceutical ingredients (APIs), preventing dosage variations. Furthermore, its inherent function as a highly efficient disintegrant facilitates rapid tablet breakdown upon ingestion, significantly enhancing API absorption rates. The low hygroscopicity of MCC also minimizes moisture uptake during prolonged storage, thereby safeguarding the shelf-life and efficacy of moisture-sensitive pharmaceutical formulations.
For food and beverage manufacturers, Microcrystalline Cellulose (MCC) serves as a high-performance food stabilizer, effectively preventing phase separation in emulsions like ice cream, dressings, and ready-to-drink beverages. As a versatile food thickener, it enhances mouthfeel and structural integrity in sauces, baked goods, and dairy items without altering the original flavor profile. Functioning as an insoluble dietary fiber, it promotes digestive health while contributing zero calories—making it an ideal ingredient for formulating low-sugar, weight-management, and diabetic-friendly consumer products. In the dietary supplement industry, MCC acts as an inert, neutral carrier, ensuring that sensitive active ingredients are evenly dispersed and easily processed into powders, granules, or capsules.
To maintain its optimal physical properties, Microcrystalline Cellulose (MCC) requires strict moisture-proof storage. It should be stored in a cool, dry, and well-ventilated environment within tightly sealed original containers to prevent moisture absorption and subsequent clumping. Excessive humidity can compromise its flowability, compressibility, and overall functional performance. Additionally, the material should be kept away from direct sunlight, strong odors, and extreme heat sources to preserve its crystalline integrity and high purity over its designated shelf life.
When integrating Microcrystalline Cellulose (MCC) into new formulations, it is crucial to follow industry best practices and ensure alignment with regional USP standards, EP standards, or FCC standards depending on the target market. For specialized pharmaceutical or nutraceutical applications, formulation engineers should carefully select the appropriate MCC grade (e.g., MCC 101 for wet granulation, MCC 102 for direct compression). Different grades offer distinct particle sizes, bulk densities, and flow characteristics tailored to specific manufacturing requirements, such as optimizing tablet hardness or enhancing powder flow in high-speed capsule filling machines.
Yes, Microcrystalline Cellulose (MCC) is universally recognized as a safe and non-toxic ingredient for both food and pharmaceutical applications. It strictly complies with USP standards, EP standards, and FCC standards, and holds approval from major global regulatory bodies for widespread inclusion in consumable products, dietary supplements, and medications.
Absolutely. Because it is derived directly from natural plant cellulose and resists digestion in the human small intestine, Microcrystalline Cellulose (MCC) is officially classified as an insoluble dietary fiber. It is frequently incorporated into food and nutritional supplements to enhance dietary fiber content, support digestive health, and assist in low-calorie product formulation.
No, Microcrystalline Cellulose (MCC) is completely insoluble in water and organic solvents. However, it exhibits exceptional dispersibility. When mechanically sheared or mixed into liquids, it forms a highly stable, three-dimensional colloidal suspension. This unique property is exactly what makes it so effective as a stabilizer and thickener in aqueous food systems and liquid pharmaceutical suspensions.
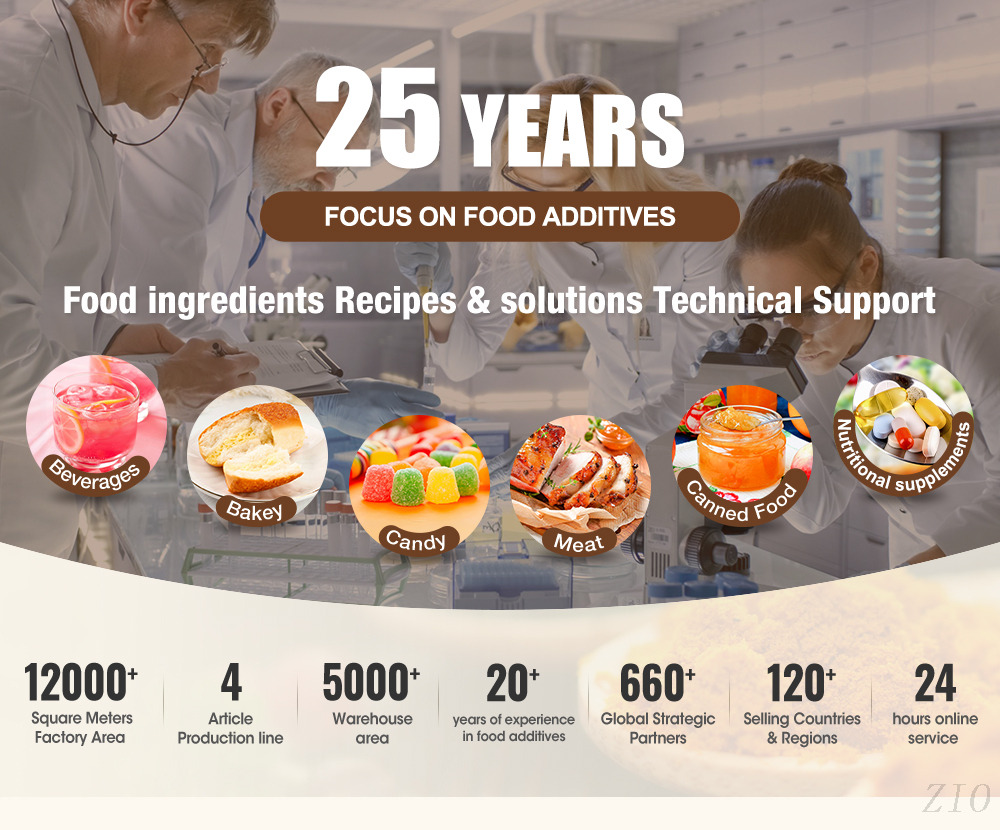
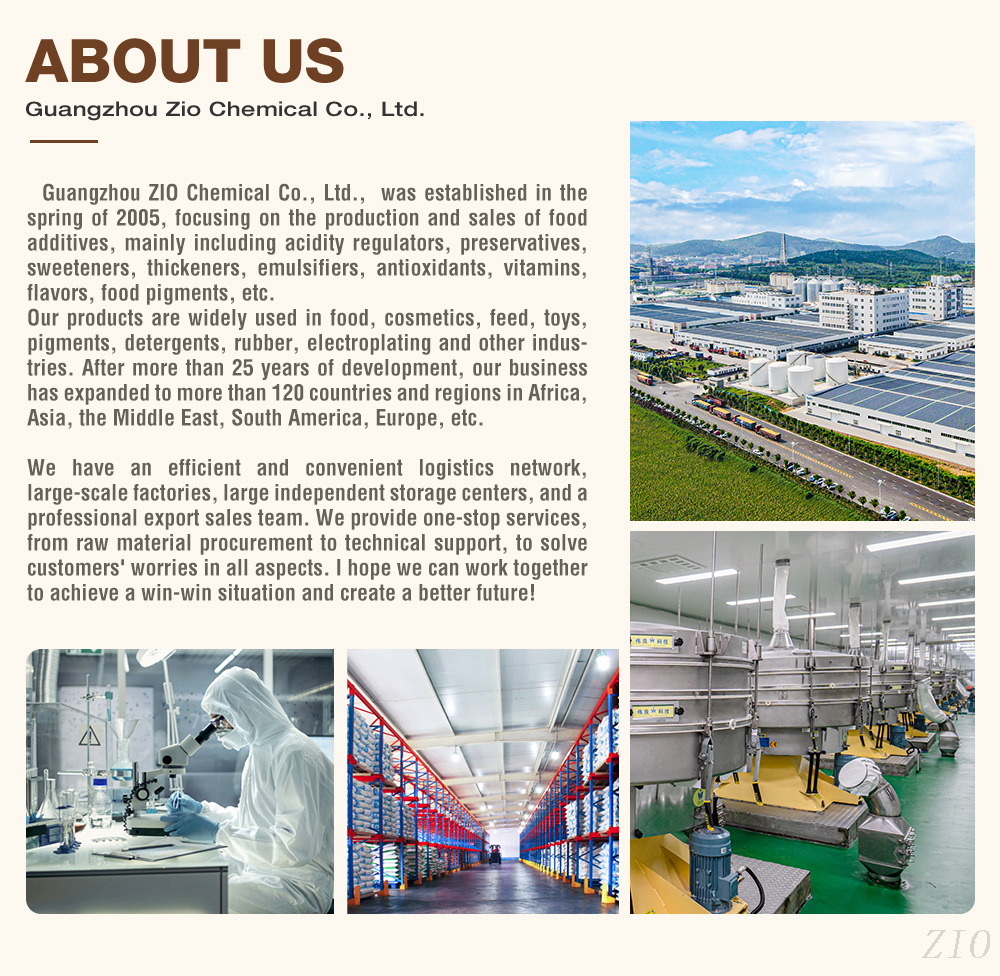
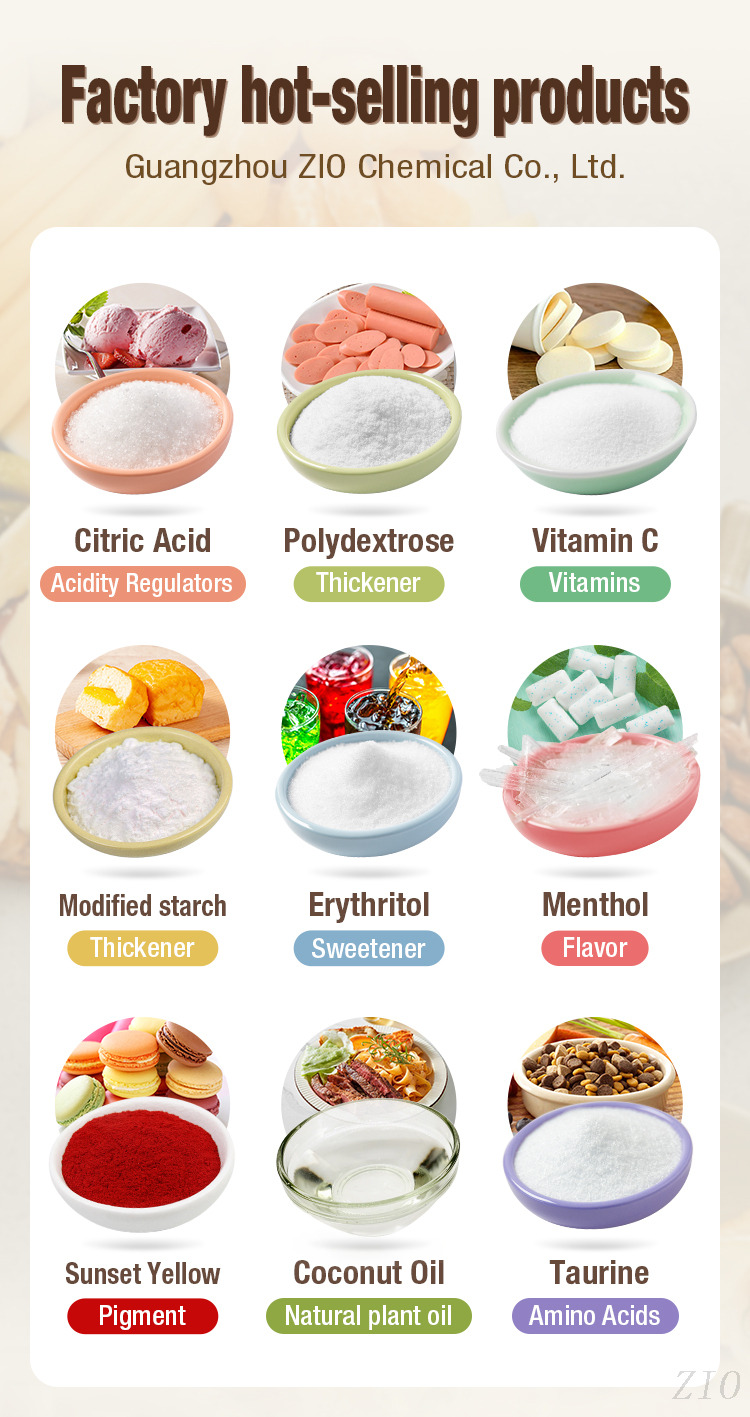
Established in the spring of 2005, Guangzhou ZIO Chemical Co., Ltd. is a specialized manufacturer and global supplier focusing on food additives and ingredients. Our comprehensive portfolio includes acidity regulators, preservatives, sweeteners, thickeners, emulsifiers, antioxidants, vitamins, flavors, and food pigments. Beyond the food and beverage sector, our reliable ingredients are widely utilized in cosmetics, feed, toys, pigments, detergents, rubber, electroplating, and various other industrial applications.
Over the past two decades of steady development, we have built a stable international presence, expanding our export business to over 120 countries and regions across Africa, Asia, the Middle East, South America, Europe, and Oceania. We operate a highly efficient logistics network, supported by large-scale manufacturing facilities, extensive independent storage centers, and a dedicated export sales team. We offer comprehensive one-stop procurement services—from strict raw material sourcing to formulation technical support—helping global clients streamline their supply chain and reduce procurement risks. We look forward to establishing long-term cooperation and creating a mutually beneficial future with you.
12,000+ Square Meters Factory Area for stable production capacity.
5,000+ Square Meters Independent Warehouse ensuring sufficient stock.
4 Advanced Production Lines dedicated to ingredient manufacturing.
20+ Years of Industry Experience in food additives.
660+ Global Strategic Partners trusting our supply chain.
120+ Exporting Countries & Regions covered.
24-hour online professional service for timely assistance.
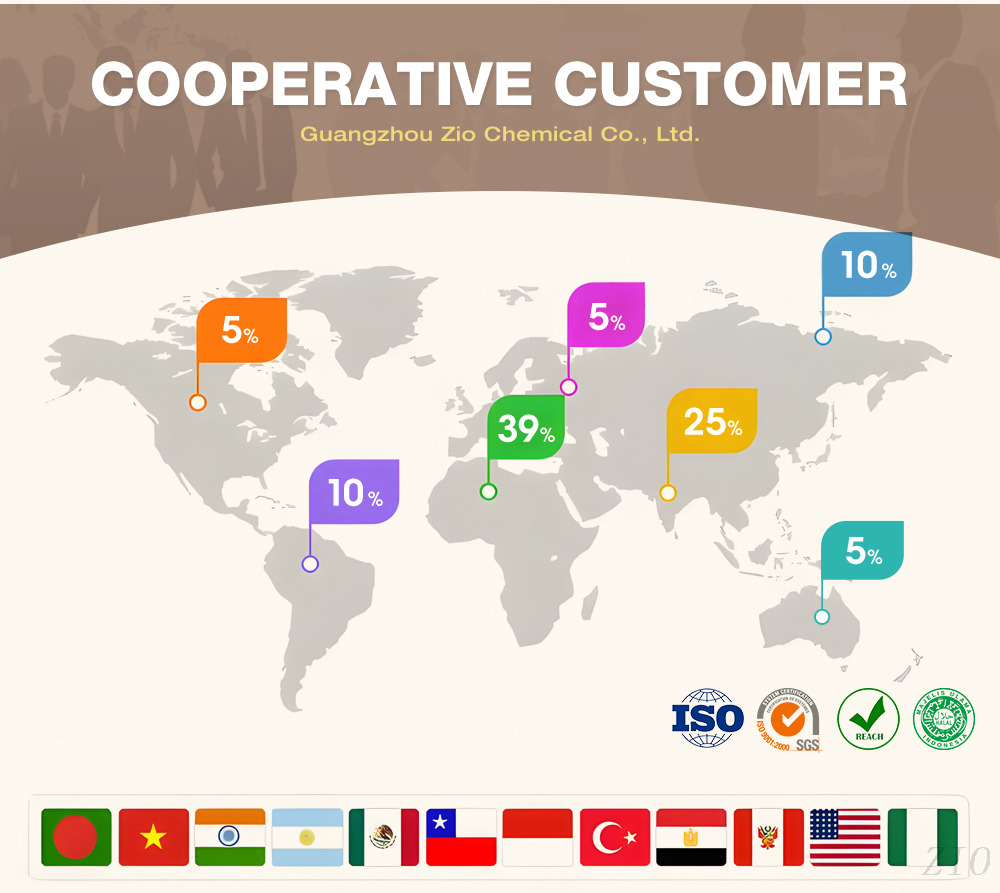
Our primary cooperation regions are: Africa (39%), Asia (25%), Europe (15%), South America (10%), Oceania (5%), and North America (5%).
Our key partner countries include South Africa, Ghana, Vietnam, the United Kingdom, Russia, Panama, Australia, and the United States, demonstrating our adaptability to diverse regional market standards.
We proudly cooperate with leading Fortune Global 500 and publicly listed companies, including AJINOMOTO, Mengniu, Nestlé, Unilever, ADM, VITA, Danone, Sunner Food, Xiwang Food, Cargill, Fonterra, and Tate & Lyle. These enduring partnerships serve as a strong testament to our product reliability, strict quality control, and global industry recognition.
Every year, our team actively participates in multiple prestigious international trade shows around the world—from Mexico, Russia, and Vietnam to major cities across China such as Shanghai and Guangzhou. These exhibitions allow us to connect face-to-face with global partners, understand regional procurement needs, and present our newest ingredient innovations to the international market.
We strictly comply with international food safety and quality management systems. Our facilities and products have obtained critical certifications, including ISO, HACCP, and Halal. These credentials demonstrate our unwavering commitment to manufacturing safety, consistent quality, and adherence to rigorous global standards, ensuring buyers can source with confidence.
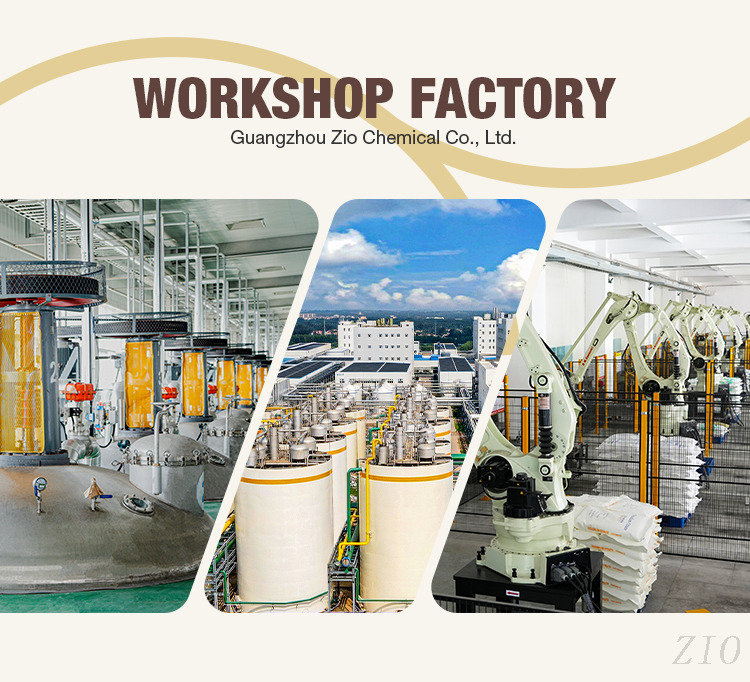
Our production workshop for food additives is modern, hygienic, and fully equipped with advanced machinery specifically designed for the safe handling and processing of food-grade ingredients. We strictly adhere to GMP standards and relevant food safety regulations to ensure the highest level of product safety. Our factory workflow encompasses every critical step: from careful raw material sourcing and precise formulation mixing to rigorous quality inspection, final packaging, and logistics. This meticulous process guarantees that our food additives consistently meet international standards and fulfill specific customer requirements.
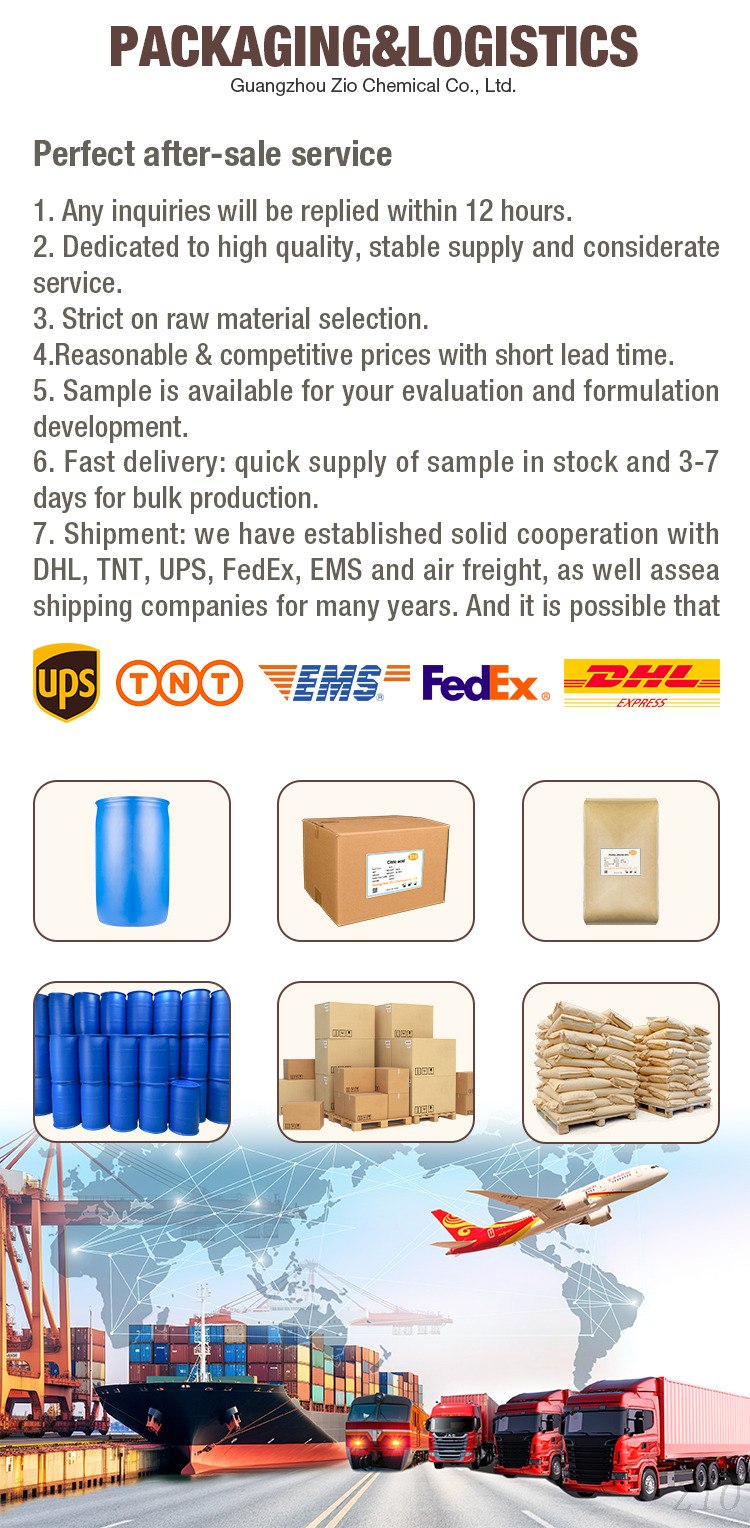
Guangzhou ZIO Chemical Co., Ltd. is committed to providing comprehensive after-sale service and reliable logistics support to ensure a smooth procurement experience.
Any inquiries or technical questions will be replied to within 12 hours.
Dedicated to maintaining consistent quality, stable supply capacity, and considerate customer service.
Strict quality control protocols applied to all raw material selection.
Reasonable and competitive pricing structures combined with short lead times.
Samples are available for your evaluation, testing, and formulation development.
Fast delivery: Quick supply of in-stock samples and a 3-7 days lead time for bulk production orders.
Reliable shipment: We have established solid, long-term cooperation with leading carriers like DHL, TNT, UPS, FedEx, and EMS for air freight, as well as major sea shipping companies for global ocean freight.
Versatile packaging types available, including customized bags, cartons, and barrels to suit your specific storage and handling needs.
We usually accept T/T, Western Union, MoneyGram, or PayPal, depending on the order size and client preference.
Delivery time depends on the order quantity. Usually, we will arrange shipment within 3 to 20 days after order confirmation.
We typically provide standard packaging of 25 kg per bag or carton. If you have special packaging requirements for your facility, we will adjust and customize it according to your needs.
Our professional sales manager will contact you within 24 hours to assist with your procurement requirements.
The shelf life depends on the specific products you order, but it is usually 2 years under proper storage conditions.
We usually provide a Commercial Invoice, Packing List, Bill of Lading, COA (Certificate of Analysis), Health Certificate, and Certificate of Origin. If your market requires any special documentation, please let us know.
Yes, we can provide a free sample once the price is agreed upon. You only need to cover the advance delivery fee for the sample shipment.
Our primary loading port is usually Huangpu Port in Guangzhou, ensuring convenient and efficient global shipping.