Sorbitol Liquid is a versatile and widely used sugar alcohol that serves as a sweetener, humectant, and texturizing agent in various industries. This clear, viscous liquid is approximately 60% as sweet as sucrose, making it an ideal low-calorie alternative for sugar in food and beverage applications. Sorbitol is favored not only for its sweetness but also for its ability to retain moisture, enhancing the texture and shelf life of products. It is commonly found in sugar-free candies, baked goods, and dietary supplements, as well as in pharmaceutical formulations such as syrups and chewable tablets. Additionally, its non-cariogenic properties make it a preferred choice in dental care products, contributing to oral health by not promoting tooth decay. With its multifunctional properties, sorbitol liquid is essential for manufacturers aiming to create healthier, appealing products.
| Quantity: | |
|---|---|


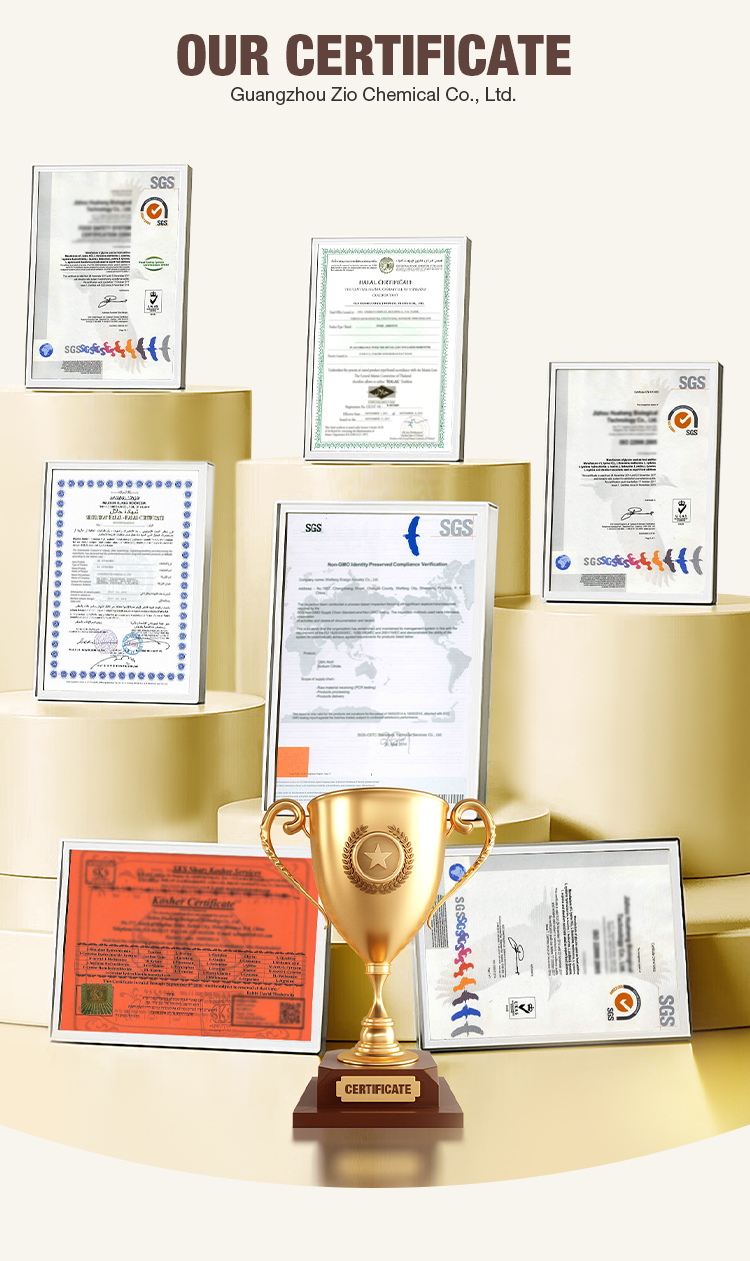
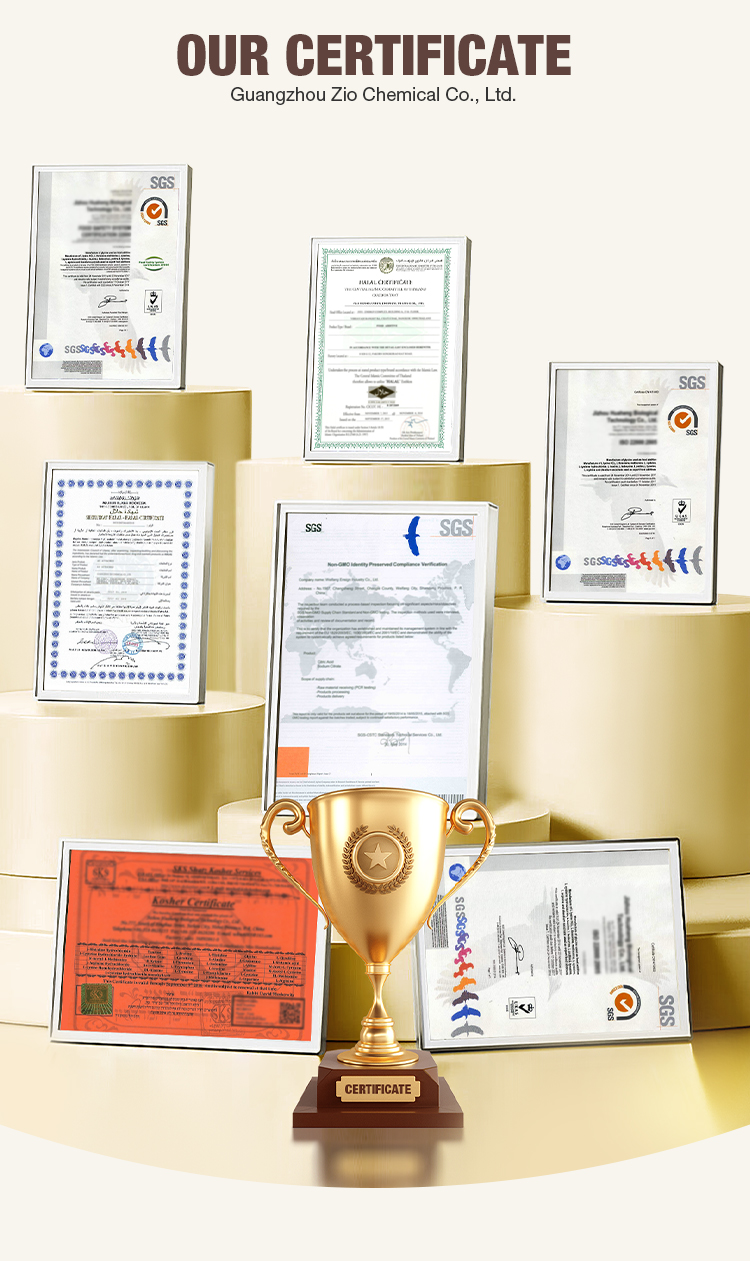
Liquid Sorbitol for Dairy (CAS No.: 50-70-4) is a highly refined polyol sugar alcohol formulated specifically to meet the rigorous demands of modern dairy processing. Presenting as a clear, viscous liquid, this stable ingredient serves as a multifunctional additive for dairy manufacturers looking to optimize product quality and production efficiency. It features a controlled solid content of 70%–75%, a balanced pH range of 5.0–7.0, and a specific gravity of 1.28–1.32 g/cm³. Designed with global compliance in mind, our liquid sorbitol strictly adheres to FCC, USP, and GB 1886.187 standards, ensuring maximum safety and consistency for large-scale procurement. Furthermore, it holds Halal (JAKIM) and Kosher (OU) certifications to support diverse market requirements. With an exceptionally low glycemic index (GI) of 9, it is an ideal formulation choice for extending shelf life, enhancing mouthfeel, and stabilizing textures in yogurt, cheese, and frozen cream products without compromising their nutritional profiles.
Shelf Life Extension: Effectively lowers water activity to inhibit microbial growth, specifically targeting yeast and mold in high-moisture dairy environments. This mechanism reliably extends the shelf life of products by 15–30 days, allowing items like commercial yogurt to increase their viable market window from 21 to 45 days, thereby reducing supply chain waste.
Low Glycemic Impact: Offering a GI of just 9 (compared to 65 for standard sucrose) and a reduced caloric value of 2.6 kcal/g, this ingredient enables manufacturers to confidently develop and label dairy items as "low-sugar" or "diabetic-friendly," meeting the growing consumer demand for healthier alternatives.
Texture Enhancement: Acts as a powerful stabilizing agent that improves the perceived creaminess in low-fat yogurt formulations by up to 35%. It also significantly mitigates syneresis (the unwanted separation of whey), ensuring a visually appealing, uniform consistency in products like cottage cheese and sour cream.
Freeze Stability: Essential for frozen dairy desserts, it effectively depresses the freezing point and prevents the formation of large, gritty ice crystals. This ensures the product maintains a smooth, premium texture even during prolonged storage and transportation at -18°C.
Cost Efficiency: Provides a highly economical alternative to other humectants. It operates at an approximately 30% lower cost than glycerin while delivering equivalent moisture-retention and texturizing properties in complex dairy formulations.
Yogurt & Fermented Milks: Typically added at a rate of 2%–5% during the post-fermentation stage. This precise integration reduces whey separation by up to 80% and significantly enhances the overall mouthfeel, all without altering the natural, tangy flavor profile expected by consumers.
Cheese Products: Recommended for incorporation at 1%–3% in spreadable items like cream cheese and processed cheese blocks. It dramatically improves spreadability right out of the refrigerator and prevents the product from hardening or cracking during prolonged cold storage.
Ice Cream & Frozen Yogurt: Utilized at 3%–6% to carefully lower the freezing point by 2°C–3°C. This targeted adjustment reduces the melting rate upon serving and significantly improves scoopability straight from the freezer, elevating the end-user experience.
Dairy Drinks: Easily mixed into protein shakes, flavored milks, and nutritional beverages at a dosage of 1%–2%. It provides a clean, mild sweetness while actively preventing protein aggregation and settling over the product's shelf life.

Q: Does liquid sorbitol affect probiotic viability in active yogurt cultures?
A: No, it is highly compatible with active cultures. Formulation studies demonstrate that it preserves ≥90% of essential probiotics, including Lactobacillus bulgaricus and Streptococcus thermophilus, throughout a standard 30-day refrigerated storage period.
Q: What is the functional difference between the 70% and 75% solid content grades for dairy?
A: The 70% grade is generally ideal for high-moisture dairy applications such as yogurt and dairy beverages, offering easier blending and pumping. The 75% grade is better suited for low-moisture products like processed cheese, where minimizing added water is crucial for structural integrity. Both grades maintain excellent stability across a wide pH range of 4.0–8.0.
Q: How should procurement and production teams handle and store liquid sorbitol?
A: It should be stored in dedicated stainless steel tanks at a controlled temperature of 20°C–30°C to prevent any unwanted increase in viscosity, which could affect pumping efficiency. It is important to avoid direct contact with copper equipment. When kept sealed under these optimal conditions, the shelf life is guaranteed for 24 months.


Product Information
| Name | Sorbitol |
| Ingredient | Sorbitol liquid |
| Specification | 270kg/drum |
| Capacity | 280.000 kg |
| Place Of Production | Guangdong, China |
| Shelf Life | 1 Year |
| Storage Conditions | Keep Shade |
When formulating high-quality food, beverage, and cosmetic products, selecting the right functional ingredients is critical to achieving the desired texture, stability, and nutritional profile. Our Liquid Sorbitol serves as a highly versatile polyol (sugar alcohol) that provides manufacturers with a reliable solution for sugar reduction, moisture control, and product stabilization. Below are the core physical and chemical advantages that make this ingredient an essential addition to your formulation strategy.
Liquid sorbitol offers a mild, pleasant sweetness that is approximately 60% as sweet as standard sucrose. This specific sweetness level allows manufacturers to significantly reduce the overall sugar content in their formulations without sacrificing the foundational taste profile that consumers expect. Unlike some high-intensity artificial sweeteners that can leave a bitter or metallic aftertaste, sorbitol provides a clean, smooth, and slightly cooling sensation on the palate. Furthermore, it functions effectively as a bulk sweetener, meaning it replaces the physical volume and mouthfeel of sugar, ensuring that the final product maintains its structural integrity and sensory appeal.
One of the most valuable functional traits of this liquid is its performance as a powerful humectant. By effectively binding water molecules, it reduces water activity within the product matrix. This moisture-retaining capability is particularly beneficial in baked goods, confectionery, and cosmetic formulations. In food applications, it prevents staleness, drying out, and crystallization, thereby maintaining a soft, fresh, and appealing texture over a longer period. For manufacturers, this translates to reduced waste and a consistently high-quality consumer experience from the production line to the end of the product's shelf life.
Maintaining formulation stability through rigorous processing conditions is a common challenge in industrial manufacturing. Sorbitol is inherently chemically stable and highly resistant to heat, meaning it can withstand high-temperature processing such as baking, pasteurization, and extrusion without degrading. Additionally, it does not participate in Maillard browning reactions unless specifically combined with certain amino acids under controlled conditions, ensuring that products retain their intended color and flavor profiles. This robust stability is crucial for commercial products requiring extended shelf lives, helping to minimize the risk of physical or chemical changes during long-term storage and distribution.
Unlike traditional fermentable carbohydrates and sugars, sorbitol is non-cariogenic, meaning it does not contribute to tooth decay. The bacteria naturally present in the human mouth cannot readily metabolize this sugar alcohol, which prevents the production of harmful plaque acids that demineralize tooth enamel. This distinct advantage makes it an exceptionally safe and highly sought-after sweetening option for oral care products, sugar-free chewing gums, and pediatric formulations. Incorporating this ingredient allows brands to confidently market their products with tooth-friendly claims, adding significant value for health-conscious consumers.
As global consumer demand shifts toward healthier dietary choices, ingredients that support metabolic wellness are increasingly important. Sorbitol features a very low glycemic index (GI) because it is absorbed slowly and incompletely in the digestive tract. Consequently, it has a minimal impact on blood glucose and insulin levels compared to standard sugars. This physiological characteristic makes it highly suitable for developing diabetic-friendly, low-carbohydrate, and keto-aligned product lines. By utilizing liquid sorbitol, manufacturers can cater to a rapidly expanding demographic of consumers who are proactively managing their sugar intake without compromising on taste or texture.
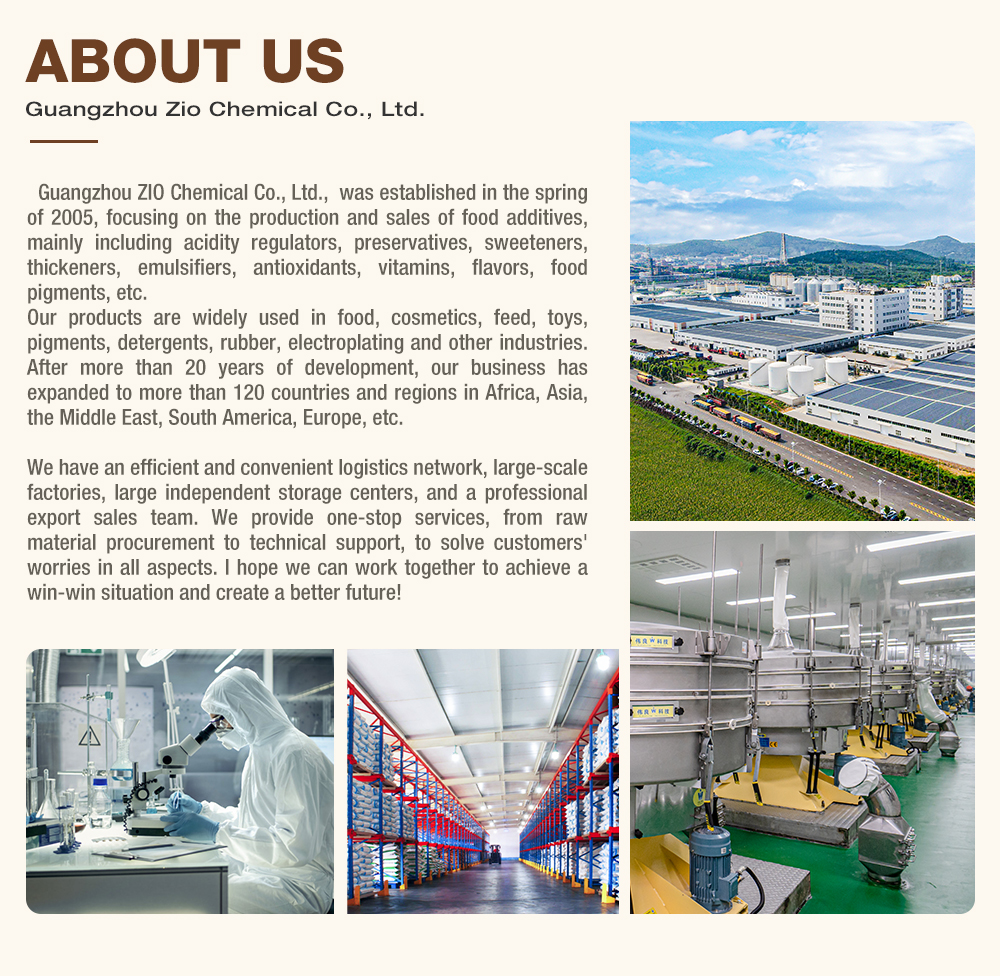
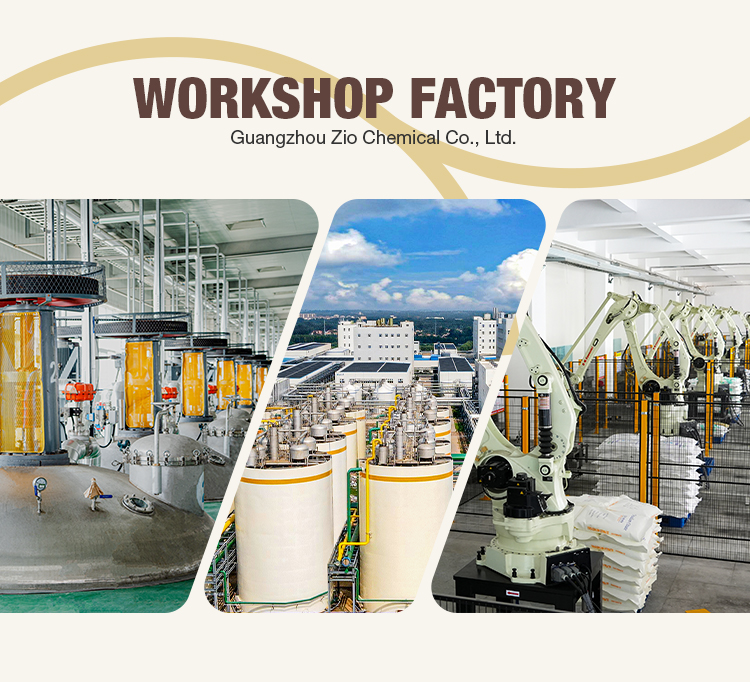
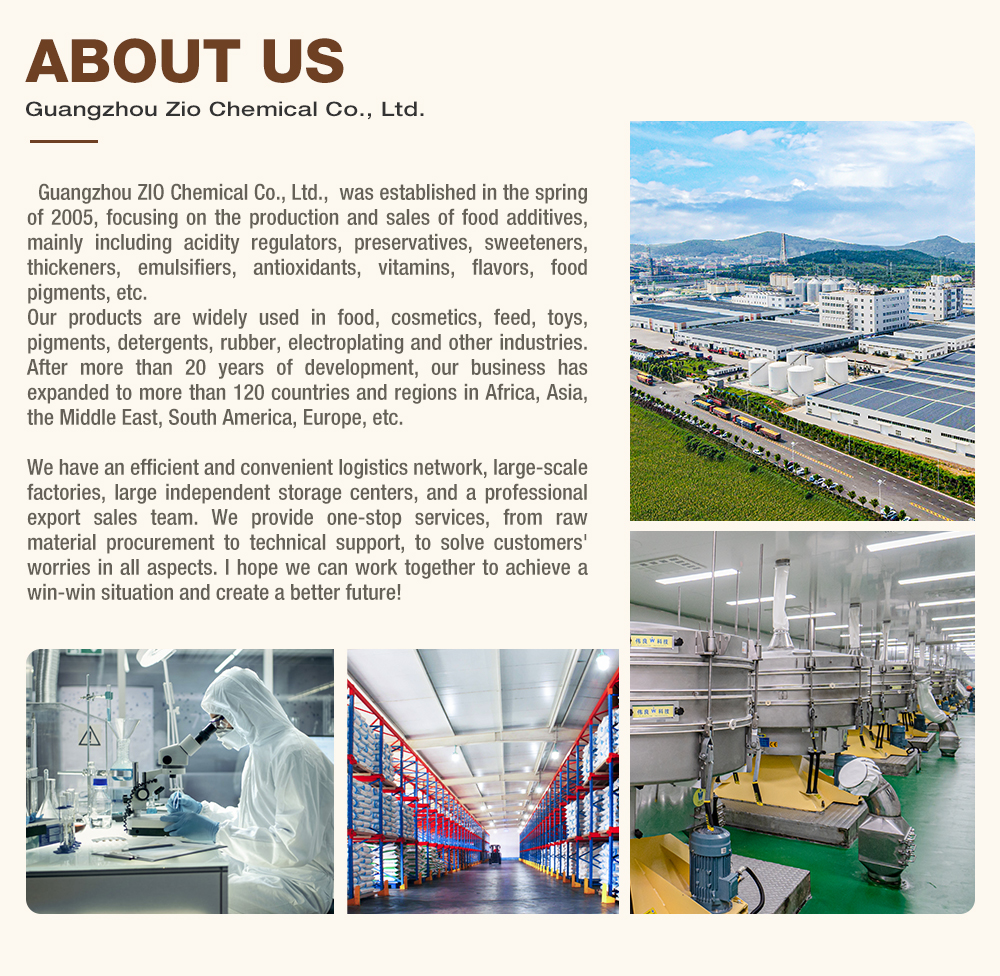
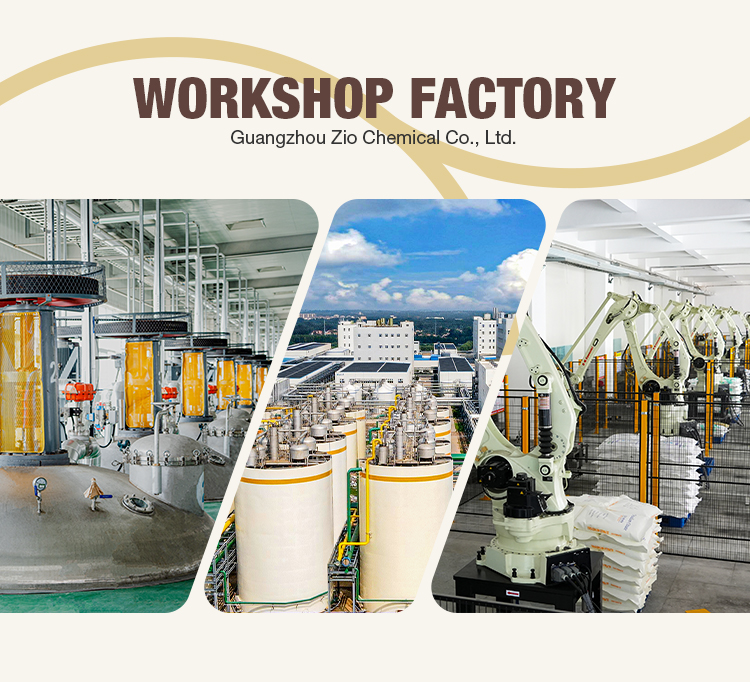
The following gallery provides a detailed visual overview of our product details, manufacturing capabilities, and quality control processes. These images reflect our commitment to maintaining high production standards and ensuring reliable supply chain solutions for our global partners.